

A fastener is a hardware device that mechanically joins two or more components together, either permanently or in a way that lets the joint be taken apart again. Bolts, screws, nuts, washers, rivets, anchors, and pins all sit inside that definition. Engineers, buyers, and maintenance teams look up the term for the same practical reason: joints fail when the fastener was wrong for the load, the environment, or the assembly method. This guide defines what a fastener is, maps the main fastener types and applications, and gives you a selection framework you can apply straight to a drawing.

What Is a Fastener?
A fastener is any hardware device that joins two or more parts by mechanical means rather than by a chemical bond such as adhesive or a metallurgical bond such as welding. The definition is wide: it covers threaded parts that create a clamping force, unthreaded parts such as rivets that lock by deformation, and retaining devices such as circlips that block movement.
The first distinction that matters is whether the joint is meant to come apart. Threaded fasteners such as bolts and screws are removable, which makes them the default whenever equipment needs servicing or disassembly for shipment. Rivets and many anchors are permanent. Picking the wrong side of that line is expensive: a permanent fastener in a serviceable joint turns a ten minute repair into a cut out and rework.
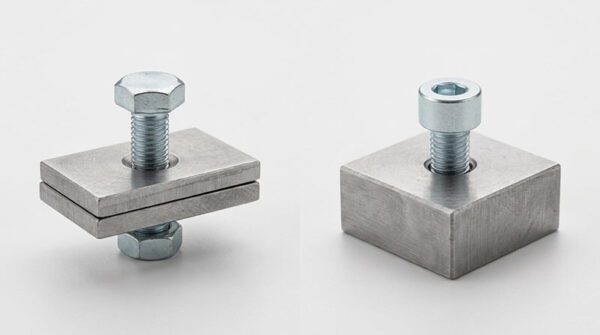
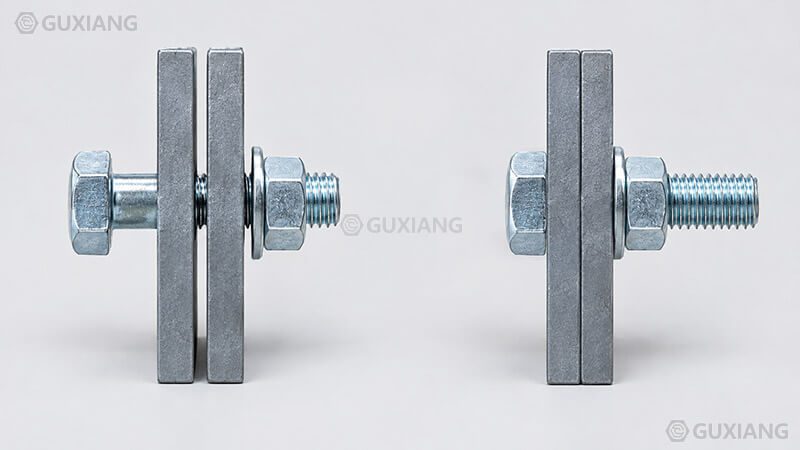
The second distinction is how the load is carried. A bolted joint works in tension: tightening stretches the bolt, and that stretch clamps the plates so friction between them resists shear. A rivet or dowel pin works in shear, and a washer works in compression, spreading load and protecting the surface. Name the load path and the fastener type follows.
Anatomy matters because drawing callouts refer to each feature by name. The head provides the bearing surface and torque interface, the shank is the unthreaded body, and the thread carries the major diameter, minor diameter, and pitch that decide whether a nut will run at all. A callout that names head style and pitch but omits thread length is a common source of rejected orders.
The overview at Wikipedia’s fastener entry uses the same framing, and the full catalog we supply lives under fasteners. Fasteners are almost always the cheapest parts in an assembly and the first blamed when it fails. That is why the definition matters commercially.
Types of Fasteners
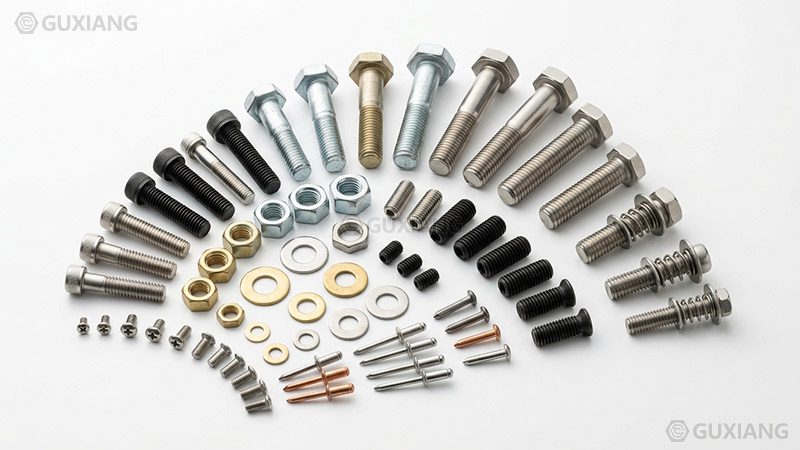
Fastener types can be sorted five ways, and a real specification touches all five. Shape and head style tells you how the part seats, drive tells you how torque gets in, thread tells you what it mates with, material tells you how long it survives, and application tells you which convention governs it.
| Type | Definition | Typical use | Pre-drilled hole required | Removability |
|---|---|---|---|---|
| Bolt | Externally threaded fastener inserted through clearance holes and tightened with a nut | Structural steel, pipe flanges, machinery frames | Yes (clearance hole) | Removable |
| Screw | Externally threaded fastener that mates with an existing internal thread or forms its own | Machine assemblies, enclosures, woodwork | Usually (pilot or clearance) | Removable |
| Nut | Internally threaded component that pairs with a bolt or stud | Any bolted joint | No | Removable |
| Washer | Flat or shaped ring that spreads load, protects the surface, or resists loosening | Under bolt heads and nuts | No | Removable |
| Set screw | Headless screw driven through a hub to lock it against a shaft | Pulleys, collars, gears | Tapped hole | Removable, semi permanent |
| Rivet | Unthreaded pin deformed on installation to form a second head | Sheet metal, aircraft skins, enclosures | Yes | Permanent |
| Anchor | Device that grips concrete or masonry by expansion, friction, or bonding | Fixing to concrete, brick, block | Yes | Removable in most designs |
Read the last two columns together, because they decide how the product behaves in service. A machine that ships in sections wants a bolt; a sealed enclosure wants a rivet.
By Shape and Head Style
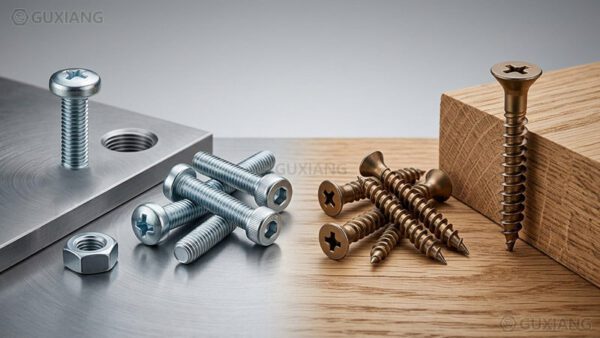
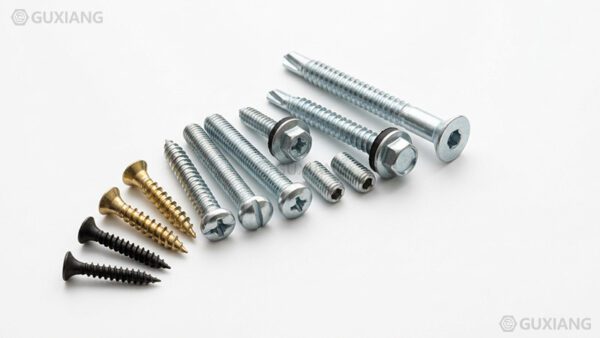
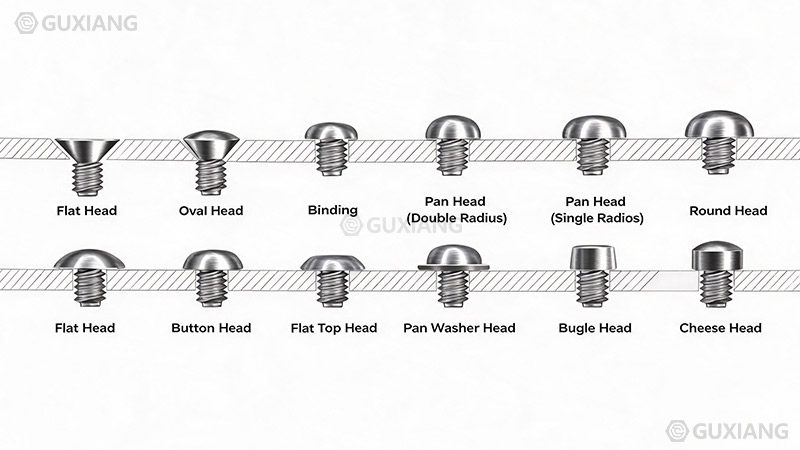
Hex heads suit structural and machinery work because a socket grips them from the side and a flange version spreads load without a separate washer. Socket cap and button heads sit low or flush, which is why they dominate enclosures where a protruding hex would foul a moving part. Countersunk heads seat flush and need a countersink. Our bolts, screws, nuts, and washers ranges are organised by this logic, and each geometry is set out in our screw head types guide.
By Drive and Recess
The drive sets how much torque a part accepts before the tool cams out. Slotted drives are the oldest and the easiest to damage. Phillips drives were designed to cam out deliberately, which protects the joint at low torque but limits the preload a technician reaches by hand. Hex and Torx transmit far more torque with less radial force, which is why Torx has taken over automotive and appliance assembly.
By Thread Form
Machine threads mate with a tapped hole or nut of the same size and pitch, and they are the form behind our machine screws. Self tapping and thread forming screws cut or roll their own mating thread in sheet metal or plastic, removing a tapping operation. Wood screws use a coarse profile with a large root radius to grip fibres without splitting. Choosing the thread form is really choosing what the substrate can take.
By Material
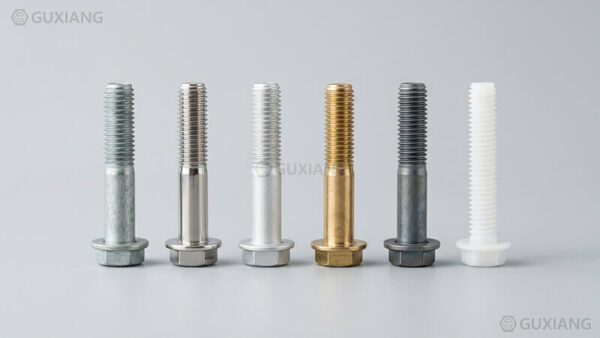
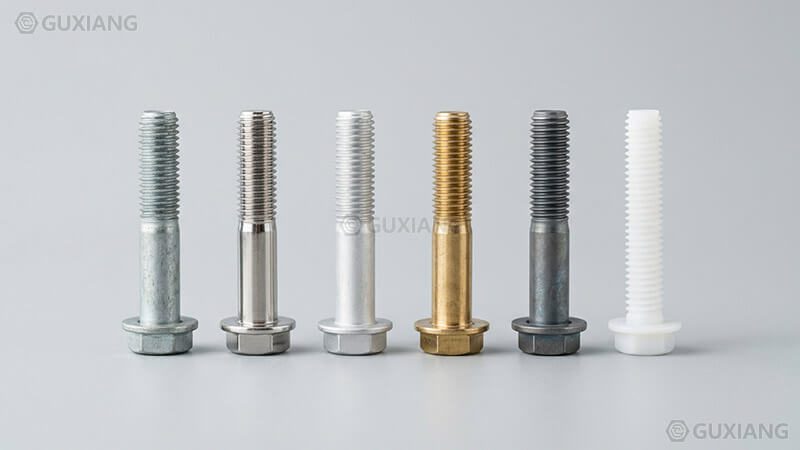
Material governs corrosion, weight, temperature, and price. Carbon steel is the default for strength per dollar, stainless buys corrosion resistance, aluminium and titanium buy weight, and plastics buy isolation.
By Application
Industry usage adds a final layer of convention. Structural steelwork defaults to heavy hex bolts with a matching nut and hardened washer. Automotive assembly defaults to flange headed screws with prevailing torque features. Electronics defaults to small machine screws into pressed or self clinching nuts.
How Do Fasteners Work?
A properly tightened bolted joint does not hold parts together by the bolt acting as a pin. It holds them by clamping. Tightening stretches the bolt elastically, that stretch is preload, and the resulting compression on the joint faces is clamp load. The plates are then held by friction between their faces, and the bolt only sees shear if that friction is overcome. This explains why a loose bolt breaks: once clamp load is gone the joint slips and the bolt takes the bending load it was never sized for. The thread geometry behind that stretch is described at Wikipedia’s screw thread entry.
The industry rule of thumb splits the input roughly 50 percent to friction under the head, 40 percent to friction in the threads, and only about 10 percent into useful preload. A change in lubrication, plating, or surface finish can therefore move achieved preload by tens of percent at unchanged torque, which is why a torque figure quoted without a friction condition is not a specification. Our metric bolt torque chart gives starting values for common grades and finishes.
Thread engagement length quietly decides whether a joint holds. A working rule for a steel screw into steel is engagement of about one times the diameter, rising to 1.5 times for aluminium and two times or more for plastics. Below that the thread strips before the bolt reaches proof load. On the bench this looks like a fastener quality problem; it is really a tapped hole depth problem.
Failure in service is rarely a single overload. Self loosening comes from transverse vibration that lets the nut rotate back a fraction per cycle, which is why prevailing torque nuts, wedge lock washers, and thread locking compounds appear in vibration prone assemblies. Relaxation comes from embedding, where surface asperities flatten and the joint loses preload. Fatigue follows once clamp load is lost. Protect clamp load: torque to a stated value with a stated friction condition, then re check after the first thermal cycle.
One practical trap is treating torque as the goal rather than the means. A torque wrench sets a target input, but the output that matters is the stretch in the bolt and the clamp it creates, and that output swings with lubrication, plating, and surface finish. The same torque on a dry plain bolt and a waxed plated bolt can land at very different preload, which is why critical joints quote torque with a friction condition or specify a tension controlled method. When the joint is safety related, verify preload directly with a skidmore or ultrasonic measurement rather than trusting the wrench alone. Document the friction condition on the drawing so the assembler and the inspector read the same number.
Fastener Materials
Material selection sets corrosion behaviour, weight, temperature limit, and unit cost in one decision. The table compares the seven families most buyers meet; treat the figures as indicative. Each family has a dedicated guide in our fastener materials comparison.
| Material family | Typical grades | Tensile strength (indicative) | Corrosion resistance | Cost index (carbon = 1.0) |
|---|---|---|---|---|
| Carbon steel | 4.6, 5.8, 8.8 | 400–800 MPa | Poor, needs a coating | 1.0 |
| Alloy steel | 10.9, 12.9, ASTM A193 B7 | 1000–1200 MPa | Poor, needs a coating | 1.3 |
| Stainless steel | A2-70 (304), A4-70 (316), A4-80 | 500–800 MPa | Good to excellent | 3.0–4.0 |
| Brass | C36000, CZ121 | 300–500 MPa | Good, not in chlorides | 3.0 |
| Aluminium | 6061-T6, 7075-T6 | 310–570 MPa | Good, from the oxide film | 2.5 |
| Titanium | Grade 2, Grade 5 (Ti-6Al-4V) | 340–1100 MPa | Excellent, including seawater | 10 and above |
| Plastic (nylon, PEEK) | PA66, PEEK, PVDF | 50–90 MPa | Excellent | High per kilogram, low per part |
Values are indicative and approximate. Confirm against the governing material and grade standard before specification.
Carbon steel is where most projects start, because it delivers the best strength for the money. The weakness is corrosion: bare carbon steel rusts as soon as it sees moisture, so most outdoor applications depend on a coating. See our carbon steel fasteners guide.
Alloy steel pushes strength higher, reaching property classes 10.9 and 12.9 with tensile approaching 1000 to 1200 MPa. It earns its place where joint size is fixed, but it corrodes like carbon steel and needs hydrogen relief after plating. See our alloy steel fasteners guide.
Stainless resists corrosion through a chromium rich passive film that reforms when damaged, so it needs no coating in many wet environments. The two families buyers meet most are 304 (A2) and 316 (A4), which adds molybdenum for chloride resistance. Grades are set out in our stainless steel fastener grades guide.
Brass serves decorative and electrical roles. It machines beautifully and conducts well enough for terminals, but it is soft beside steel and suffers in chloride service. Specify it for appearance, not structure.
Aluminium fasteners carry roughly one third the density of steel, so they appear in transport, aerospace, and electronics enclosures where mass is the constraint. The oxide film gives corrosion resistance and anodizing thickens it, but strength is modest. Detail is in our aluminium fasteners guide.
Titanium offers outstanding strength to weight and seawater corrosion resistance, earning aerospace and marine duty where steel would rust and aluminium would be too weak. Cost is typically an order of magnitude above steel, so it stays a specialist choice.
Engineered plastics such as nylon and PEEK produce parts that are non conductive and non magnetic, suiting electrical and corrosive service at a fraction of metal strength. Our nylon and PEEK fasteners guide explains where they fit.
One rule overrides the rest on mixed metal assemblies: do not couple metals far apart on the galvanic series without isolation. A small aluminium bracket on a large stainless panel is the classic failure, because the aluminium becomes the anode. Fixes include an isolating washer, a coating barrier, or closer partners. The mechanism is set out at Wikipedia’s galvanic corrosion entry.
Fastener Standards
Standards exist so a callout on a drawing means the same thing to a mill in one country and an assembly plant in another. In practice a specification cites two documents: a dimensional standard that fixes the geometry, and a material or property standard that fixes the strength. A structural hex bolt callout cites ASME B18.2.1 for dimensions and ASTM A325 or F3125 for material.
| Body or system | Region | Typical fastener standards | What it governs |
|---|---|---|---|
| ISO | International | ISO 4014, ISO 4032, ISO 898-1, ISO 3506 | Metric dimensions and property classes |
| DIN | Germany, widely adopted across Europe | DIN 931, DIN 934, DIN 912 | Metric dimensions, largely replaced by ISO |
| ANSI / ASME | United States | ASME B18.2.1, B18.2.2, B1.1 | Inch series dimensions and thread form |
| ASTM | United States, cited globally | A307, A325, A490, F3125, A193, F593 | Material and performance requirements |
| SAE | United States, automotive led | SAE J429, J995 | Inch series strength grades |
The systems overlap more than newcomers expect, and that is where substitution mistakes happen. DIN 931 and ISO 4014 describe nominally the same hex bolt but differ on width across flats for some sizes. Metric and inch series are not interchangeable at all, because thread angle and pitch differ even at similar diameters. Name one system per drawing.
Standards are maintained by the bodies that publish them, and the most durable links point at the organisations. Start with ISO for international metric work, ASTM International for North American material and coating specifications, ASME for inch series dimensions, and SAE International for automotive grades. For how the DIN, ISO, ANSI, and ASME systems relate on a global project, see our fastener standards explained guide.
Fastener Dimensions and Sizes
A size callout is four numbers in the right order: nominal diameter, thread pitch, length, and the standard that fixes head and thread geometry. “M10 x 1.5 x 50 ISO 4014” is unambiguous. “M10 x 50” is not, because M10 also comes in 1.25 and 1.0 fine pitches, and a fine pitch nut will start on a coarse bolt and seize a few turns down. Length conventions differ too: hex bolt length excludes the head, countersunk screw length includes it.
| Metric designation | Nominal diameter (mm) | Standard coarse pitch (mm) | Hex across flats (mm) |
|---|---|---|---|
| M3 | 3.0 | 0.5 | 5.5 |
| M4 | 4.0 | 0.7 | 7 |
| M5 | 5.0 | 0.8 | 8 |
| M6 | 6.0 | 1.0 | 10 |
| M8 | 8.0 | 1.25 | 13 |
| M10 | 10.0 | 1.5 | 16 |
| M12 | 12.0 | 1.75 | 18 |
| M16 | 16.0 | 2.0 | 24 |
| M20 | 20.0 | 2.5 | 30 |
| M24 | 24.0 | 3.0 | 36 |
Common ISO metric coarse series. Fine pitch and inch series dimensions differ; confirm against the dimensional standard.
Inch series fasteners use a different vocabulary: fractional diameters, threads per inch, and gauge numbers for small screws. A 1/2-13 UNC bolt and an M12 bolt are close in diameter but not interchangeable, because 13 threads per inch is not a 1.75 mm pitch. Convert deliberately and check the thread form, not only the diameter.
Three checks save most rejected batches. Confirm across flats against your socket, because ISO and DIN differ on some sizes. Confirm the pitch against the mating part rather than assuming coarse. Confirm the thread length, because fully threaded and partially threaded bolts are not substitutes in a joint that relies on the shank for shear. Full listings sit in our metric thread chart and imperial thread chart.
A tolerance class is part of the size callout even when it is left unstated. Metric threads default to 6g on the bolt and 6H on the nut, a deliberate clearance that lets the fastener assemble and still carry load. A coarse pitch gives more thread engagement per turn and resists cross threading, so it is the default for general assembly; a fine pitch takes up less length for the same tension and holds better under vibration, which is why thin sections and adjustment screws use it. Length is measured to a convention: hex bolt length stops at the underside of the head, while a countersunk screw length includes the head, so a 20 mm hex bolt and a 20 mm countersunk screw are not the same installed length. State the convention when the length is critical.
How to Choose a Fastener
Fastener selection is a sequence, not a single decision. Work the steps in order, because each one narrows the options for the next.
Define the joint. What is being joined, how thick is the stack, and is there access to both sides? One sided access pushes you toward blind rivets, self tapping screws, or clinch hardware.
Quantify the load. Tension, shear, or a mix, and static, cyclic, or shock? Cyclic loading makes clamp load retention the priority, which favours higher preload and a locking feature over a bigger diameter.
Set the environment. Indoor dry, rain washed, coastal salt, chemical, or high temperature each narrows the material and coating pair.
Pick the material and grade. Material for the environment, grade for the load. Our bolt grade chart sets the strength classes side by side.
Choose the coating. Match it to the environment, then check the effect on thread fit and on friction.
Fix the standard and dimensions. Name the system, head style, diameter, pitch, and length, in that order.
Check assembly and cost. Driver access, tool clearance, automation, and total installed cost rather than unit price.
The table below compresses that sequence for the service conditions we see most often.
| Service condition | Recommended type | Recommended material | Recommended coating or finish |
|---|---|---|---|
| Dry indoor, light load | Machine screw or self tapping screw | Carbon steel 4.6 / 5.8 | Zinc plate, Fe/Zn 5–8 |
| Indoor machinery with vibration | Hex bolt plus nut plus locking washer | Carbon steel 8.8 | Zinc plate, Fe/Zn 8–12 |
| Outdoor, rain exposure | Hex bolt or structural bolt | Carbon steel 8.8 | Hot dip galvanized or Fe/Zn 25 |
| Coastal air or de-icing salt | Hex bolt or screw | Stainless A4-70 (316) | Passivation |
| Chemical or food plant wash-down | Screw or bolt | 316 stainless or PEEK | Passivation, or none for polymer |
| Weight critical assembly | Titanium or aluminium bolt | Ti Grade 5, or 6061-T6 | Anodizing for aluminium, none for titanium |
| Elevated temperature service | Stud plus nut | Alloy steel A193 B7 or B8M | None, or phosphate with oil |
| Electrical isolation or non magnetic duty | Nylon or PEEK screw | PA66 or PEEK | None |
| Thin sheet with blind access | Blind rivet or self clinching nut | Aluminium or steel body | Per base metal |
| Frequent service access | Captive screw, or bolt plus washer | 8.8 or A2-70 | Zinc plate or passivation |
Indicative recommendations. Confirm against the governing design code and the actual service environment.
Two habits separate a good specification from an average one. Write the environment on the drawing alongside the part callout. Treat unit price as the last filter: a fastener that costs three times more but removes a warranty claim is usually cheaper.
Three mistakes appear repeatedly in rejected specifications. The first is rating the joint by diameter alone and ignoring engagement length, which lets the thread strip before the bolt reaches proof load. The second is specifying a coating after the threads are cut, so the plating consumes the fit and the nut jams; decide the coating before the thread is rolled. The third is mixing systems on one drawing, such as a metric bolt with an inch nut, which looks close on paper and fails on the bench. A short checklist on the drawing, diameter, pitch, grade, coating, and standard named in that order, prevents most of these before the first part is made.

Fastener Surface Treatments and Coatings
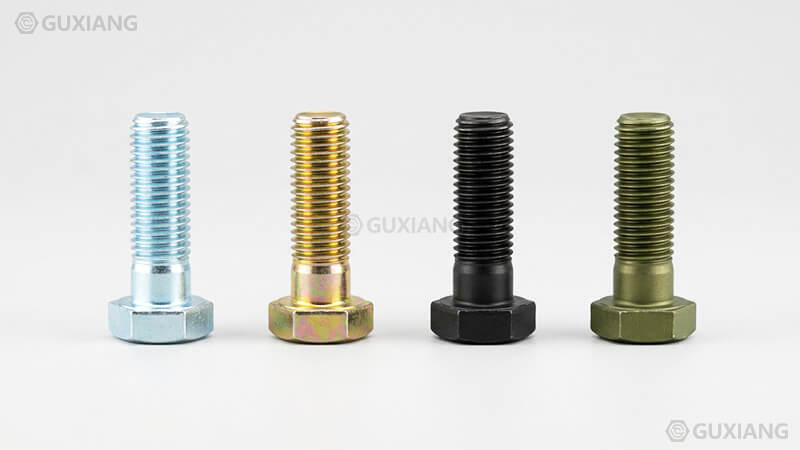
A coating lets an inexpensive carbon steel fastener survive outdoors, and the choice often decides service life more than the base metal does. The options trade thickness, cost, and thread fit, so match the coating to the environment.
| Coating | Process | Typical thickness | Indicative ASTM B117 salt spray | Relative cost | Notes |
|---|---|---|---|---|---|
| Zinc electroplating | Electrolytic | 5–25 µm | 96–240 h chromated | 1.0 | Thin and economical, holds thread fit |
| Hot dip galvanizing | Molten zinc bath | 45–85 µm on bolts | 500–1500 h | 1.5 | Thick and durable, swells threads |
| Mechanical galvanizing | Cold peening | 25–150 µm | Good | 1.5 | No hydrogen embrittlement risk |
| Zinc flake | Dip and spin | 8–25 µm | 480–1000 h | 2.0 | No hydrogen risk, high temperature tolerant |
| Black oxide | Chemical conversion | Under 1 µm | Minimal | 0.8 | Cosmetic only |
| Anodizing | Electrolytic, aluminium | 5–25 µm | Good | 1.5 | Hardens the surface |
| Passivation | Chemical, stainless | Negligible | Enhances base resistance | 0.5 | Rebuilds the passive film |
Values are indicative and approximate. Salt spray hours rank options; they are not a field life prediction.
The first shop floor issue is thread fit. A metric thread is cut to a tolerance class, 6g for the bolt and 6H for the nut, and the clearance is small by design. A plating of 8 to 25 µm can consume a large share of that tolerance, so a nut that ran freely before plating binds after it, and go/no-go gauges fail at incoming inspection. The fix must be decided before plating: tap the nut oversize, or cut or roll the thread after coating. The effect grows as diameter shrinks, so an M3 fine thread is far more at risk than an M20 coarse one.
The second issue is hydrogen embrittlement. Acid pickling and electroplating can drive hydrogen into a hardened steel part, and on high strength fasteners it can cause sudden brittle fracture after installation. The remedy is a hydrogen relief bake applied soon after plating, commonly within four hours, at roughly 190–220 °C for a minimum of three hours. Above roughly 1000 MPa tensile or 39 HRC the bake is not optional; above 1200 MPa many specifications forbid electroplating and require a process with no acid step, such as mechanical galvanizing or zinc flake. Both thresholds are laid out in ASTM B633-23.
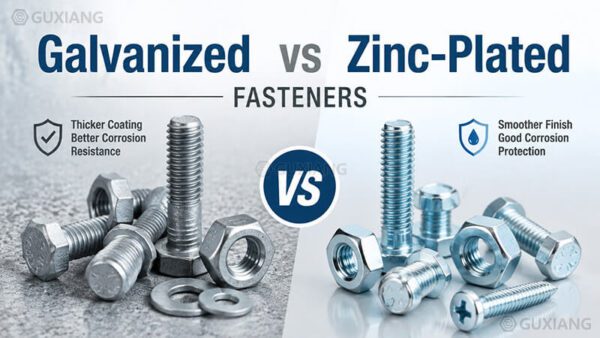
Read corrosion testing correctly as well. ASTM B117 neutral salt spray, described at ASTM B117, is a comparative laboratory method, not a service life guarantee: a part that survives 1000 hours in the cabinet can still fail quickly in a crevice. Use the hours to rank options, then validate the real joint. For the most specified finish see our zinc plating guide, and for the two zinc families our galvanized versus zinc plated comparison. Stainless takes a different route: passivation rebuilds the chromium oxide film, described at Wikipedia’s passivation entry.
Applications of Fasteners
Fastener applications are best grouped by the demands each sector places on the joint, because those demands drive the specification.
Structural steel and construction work in high clamp load on large diameters, usually with plain or galvanized carbon steel bolts in a specified grade. Slip resistant connections depend on clamp load rather than shear, so the tightening method matters as much as the part.
Automotive assembly is a different problem: very high volume, automated driving, and a hard requirement that joints do not come back. Flange headed screws with prevailing torque threads, Torx drives that will not cam out, and zinc flake coatings that carry no hydrogen risk all follow from those constraints. Weight saving adds aluminium and titanium.
Industrial machinery is the most varied category. Frames use hex bolts and washers, guards use captive screws so the panel cannot be dropped, and rotating assemblies use set screws and lock nuts. Serviceability drives most of it, because a joint a technician cannot reach is a joint left loose.
Electronics and electrical enclosures push toward small machine screws into pressed or self clinching nuts, with plastic fasteners where isolation is needed. Torque values are low and the failure mode is a stripped thread.
Marine and coastal installations are where material choice dominates. Chloride exposure defeats plain zinc quickly, so A4-70 (316) stainless or a heavy coating on carbon steel is the starting point, and dissimilar metal contact must be designed out.
Wood and furniture work uses its own family, from coarse wood screws to confirmat screws, plus deck screws with corrosion resistant coatings outdoors. The choice interacts with the substrate: our drywall screw versus deck screw comparison shows how a small geometry change moves a screw from interior board to treated timber. Aerospace adds traceability, titanium, and documented inspection. Energy and process plant adds pressure and temperature, which brings stud bolts to ASTM A193 grades.
How Fasteners Are Manufactured
Most headed fasteners start as wire rod and are formed by cold heading: the wire is cut to length and upset in a multi station machine that forces metal into a die, forming the head without cutting. Cold heading is fast, produces almost no scrap, and work hardens the material. Critically, it leaves the grain flow following the shape of the part rather than cut across it, which is why a cold headed bolt is stronger in the head to shank fillet than the same part machined from bar. Machining is reserved for large diameters, low volumes, and special geometries, because it wastes material and interrupts grain flow where fatigue cracks start.
Threads are then formed by rolling rather than cutting on almost all production fasteners. Two dies press the thread form into the blank, displacing metal instead of removing it. Rolled threads are stronger for two reasons: the surface is burnished and work hardened, and the grain flow follows the profile.
Heat treatment comes next for anything above the lowest property classes. Carbon and alloy steel fasteners are quenched and tempered to reach the specified strength and toughness, and the tempering temperature sets the balance between hardness and ductility. This step makes a 10.9 bolt a 10.9 bolt, and it also puts hydrogen embrittlement on the risk list, because a hard part is a susceptible part.
Surface treatment follows, then inspection. Thread inspection uses go/no-go gauges: the go gauge must run the full thread under finger torque, and the no-go gauge must not enter beyond the permitted amount. On a coated part the go gauge is the check that matters, because it catches a plating that has eaten the tolerance. Dimensional checks cover across flats, head height, and length; mechanical sampling covers tensile and hardness. Where we add value is treating these as one connected process, the subject of our engineering driven fastener solutions page.
Volume production holds the tolerances that matter through the tooling rather than through inspection. The cold heading die and the thread rolling dies set the geometry part to part, so a run of a million bolts stays inside the window set by the gauges, and the inspector samples rather than measures every piece. Secondary operations such as drilling a hole, milling a slot, or threading a reduced shank are added after forming when a customer needs a special feature, and each one is a point where grain flow is interrupted, so it is located away from the fillet where fatigue starts. The same part made by machining from bar would need full inspection and still carry the weaker grain structure.
Custom Fastener Options
Catalog parts cover most requirements, and the economics of cold heading mean a standard part is almost always cheaper. There are four situations where a custom fastener is worth it, and in each the tooling cost is recovered elsewhere: a geometry the catalog does not offer, such as a non standard length, shoulder diameter, or combined head and thread form; a material or grade combination the environment demands; a coating or lubrication specification that must hit a salt spray or friction target; and consolidation, where one part replaces two or three.
Custom work changes the commercial shape of the order. Tooling is a fixed cost, so unit price falls steeply with volume and there is a minimum quantity below which machining is the better route. Lead time includes tooling manufacture and first article approval, which belongs in the project schedule. First article inspection should be agreed before production, with the acceptance gauges named in writing.
The deliverable that matters most is a drawing the manufacturer can read without guessing: every dimension affecting fit, the standard, material and grade, coating and thickness, and inspection method. Our custom fastener services team works from that level of definition.
Need a specific screw size, material, standard or custom geometry?
Send the drawing and the service environment to our engineering team and we will confirm the specification, the tooling route, and a realistic lead time.
FAQ
What is the difference between a bolt and a screw?
A: A bolt is designed to be inserted through clearance holes and tightened with a nut, while a screw mates directly with a thread in one of the parts being joined or forms its own thread as it is driven. The distinction is about how it is used rather than how it looks, which is why the same externally threaded part can be called either depending on the joint. In practical terms, a bolted joint is tightened from the nut side and a screwed joint is tightened from the head side. Both create the same clamping force.
What are the main types of fasteners?
A: The main groups are Threaded fasteners, which include bolts, screws, studs, set screws, and nuts; non threaded fasteners, which include rivets, pins, anchors, and retaining rings; and auxiliary parts such as washers that support the joint. Within threaded fasteners the classification runs by head style, drive type, thread form, material, and application. Most industrial assemblies use a bolt or screw with a nut or tapped hole, plus a washer to spread the load.
What is the most common fastener material?
A: Carbon steel is the most common fastener material because it offers the best strength per unit cost and the widest availability in sizes and head styles. Its weakness is corrosion, so it is almost always supplied with a coating such as zinc plating for outdoor or humid service. Stainless steel is the next most common where corrosion resistance matters, followed by alloy steel for high strength, aluminium and titanium for weight saving, and plastics for electrical or chemical isolation.
How do I choose the right fastener size?
A: Work from the joint backwards. Measure the total stack thickness, add the nut height plus two or three threads of protrusion, and that is your minimum length. Choose the diameter from the load, using the property class to set how much clamp load the section can carry, then check the thread engagement length: around one times the diameter in steel, roughly 1.5 times in aluminium, and more in plastics. Finally confirm the pitch, because a fine pitch nut will start on a coarse thread and then seize.
What does a fastener grade number mean?
A: On metric carbon steel fasteners the grade is a property class such as 8.8 or 10.9, where the first number times 100 gives the minimum tensile strength in MPa and the second number times 10 gives the yield to tensile ratio. So an 8.8 bolt has a minimum tensile strength of 800 MPa and yields at 80 percent of that. Inch series fasteners use SAE grades such as 2, 5, and 8, and stainless uses codes such as A2-70 or A4-70, where 70 means 700 MPa tensile.
What is the difference between metric and imperial fasteners?
A: Metric fasteners are designated by a nominal diameter in millimetres and a thread pitch in millimetres, such as M10 x 1.5, while imperial fasteners use a fractional diameter and threads per inch, such as 1/2-13 UNC. The two are not interchangeable even at similar diameters, because the pitch and, in some cases, the thread angle differ. Metric parts follow ISO dimensional standards and inch parts follow ASME or SAE, so the required tools and washers differ as well.
Are fasteners and hardware the same thing?
A: Not quite. Fastener refers to a device whose primary function is to join or secure components, such as a bolt, screw, nut, washer, rivet, or anchor. Hardware is a broader trade term that can include fasteners along with brackets, hinges, handles, and other items that support an assembly without joining it. In purchasing practice the two words often overlap, and some suppliers list fasteners as a subcategory of hardware.
How do you stop a fastener from loosening?
A: Loosening from vibration happens when transverse movement lets the nut rotate back slightly on each cycle, so the fix is to keep either the preload or the relative motion. Options include a prevailing torque nut or screw, a wedge lock or serrated washer, a thread locking compound, a castellated nut with a split pin, or a safety wire in aerospace practice. Tightening to the correct preload in the first place matters more than any locking device, because a joint with enough clamp load rarely loosens on its own.
What is the difference between a permanent and a removable fastener?
A: A removable fastener, such as a bolt with a nut or a screw into a tapped hole, can be disassembled and refitted without destroying the part or the joint. A permanent fastener, such as a solid or blind rivet, a clinch nut, or a welded stud, is designed to stay in place and must be drilled out or cut away for removal. The choice depends on whether the assembly will need servicing, adjustment, or disassembly for shipping at any point in its life.
What is clamp load and why does it matter?
A: Clamp load is the compressive force that a tightened fastener applies to the joint, produced by stretching the bolt when it is torqued. It matters because a properly clamped joint transfers shear load through friction between the plates rather than through the bolt shank, which is what keeps the fastener from seeing fatigue loading. If clamp load is lost through loosening, relaxation, or embedding, the joint starts to slip and the bolt begins to carry alternating load, which is how most bolted joints eventually fail.
References
Fastener, Wikipedia. Background on the fastener family, the permanent and non permanent split, and the scope of the term used in this guide.
Screw thread, Wikipedia. Reference for thread geometry, pitch, and the mechanics behind preload generation.
ISO. The international body behind ISO 4014, 4032, 898-1, and 3506 cited in the standards and dimensions sections.
ASTM International. Source of A307, A325, A490, F3125, A193, and F593 referenced across the standards section.
ASTM B633-23, Electrodeposited Coatings of Zinc on Iron and Steel. The current revision setting zinc plating thickness classes and hydrogen relief baking requirements.
ASTM B117, Standard Practice for Operating Salt Spray (Fog) Apparatus. The neutral salt spray test method referenced for comparative coating data.
ASME. Publisher of the ASME B18 series dimensional standards and B1.1 thread form for inch series fasteners.
SAE International. Source of SAE J429 and J995 inch series strength grades for carbon and alloy steel fasteners.
AMPP. The corrosion and coatings authority, formed from NACE, referenced for coating selection and corrosion practice.
Galvanic corrosion, Wikipedia. Background on dissimilar metal attack and the galvanic series used in the materials section.
Passivation (chemistry), Wikipedia. Reference for the passive film behind stainless corrosion resistance and the passivation treatment.